Abstract
This report examines a class of manufacturing capability that statistical counting easily misses: whether equipment and supplies, once they reach the field and have been struck, broken, stored too long or frozen, can still complete their task.
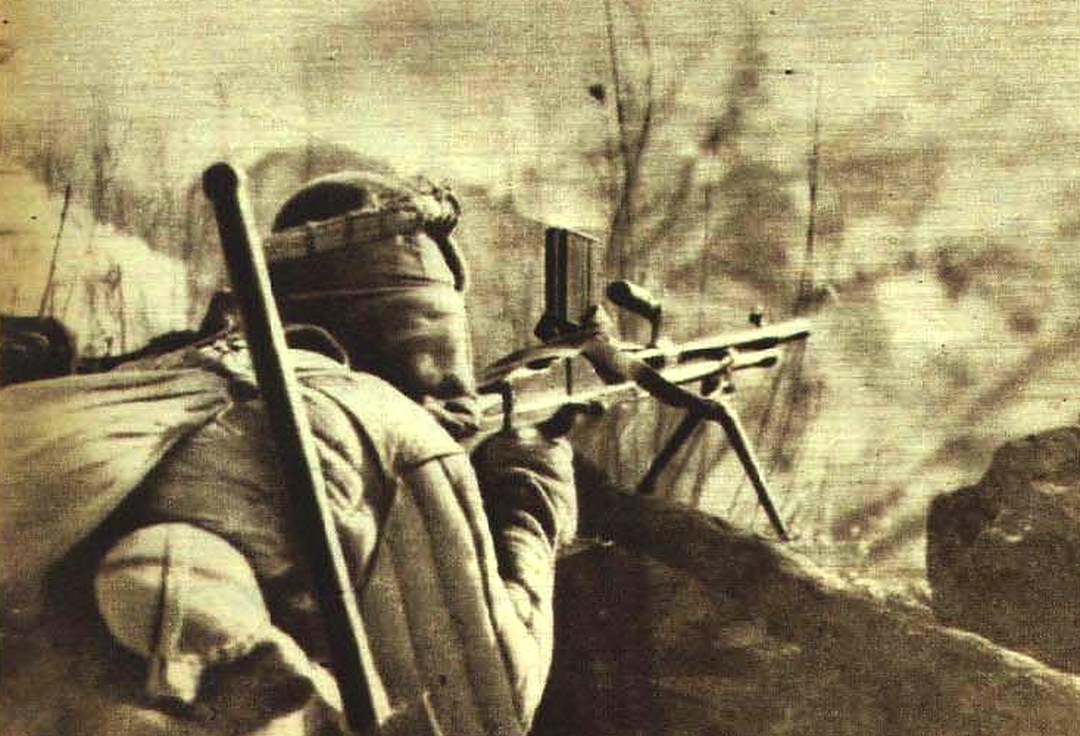
On 25 October 1950 the Chinese People's Volunteers fought their first battle after entering Korea; seventy-six years later to the day, this report was finalised. It is published on that date because all five details used here come from the three or four years that followed.
The entry point is five battlefield details. In the autumn of 1951, the Chinese People's Volunteers (CPV) moved their fortifications underground in the central part of the Korean Peninsula, and a water bucket made of thin sheet iron and scrap tyres, divided into several compartments inside, appeared in the tunnels; in 1950, a batch of radars rebuilt from captured equipment equipped the first radar battalion; in Shanghai and Shijiazhuang in the 1950s, a fermenter that would not fit changed the order in which the plant building and the equipment were built; in the winter of 1950, a handful of roasted wheat flour (chaomian) solved the problem of feeding the front line; and at the Chosin Reservoir in the same year, a winter garment pushed the conflict between warmth and moisture transmission to an extreme.
This report reconstructs each of the five details as an engineering capability, and then traces it down to the industrial supply that carries that capability today. Company counts come from the institute's enterprise records and are counted by the middle class and small class of the national economic industry classification; only companies whose operating status is normal are included, and companies the platform has added from other sources are excluded; the counts are numbers of enterprise records, not output value, not output volume and not production capacity. A single company may belong to several industry categories at once, so the figures for individual categories cannot be added together.
The main findings are as follows.
First, the five capabilities are damage tolerance, maintainability, scale-up, shelf life and environmental adaptability. What they have in common is that none of them is written on a product's factory specification sheet. A specification sheet gives dimensions, material, power, precision and certificate, and describes behaviour under standard conditions; these five describe behaviour under non-standard conditions, which is exposed only in the field and can be confirmed only through testing, verification and field data.
Second, all five capabilities are the outcome of trade-offs rather than being better the higher they are. Compartmentalisation costs volume, modularity adds connectors, scale-up sacrifices one mass-transfer metric or another, shelf life sacrifices taste or nutrition, and environmental adaptability sacrifices weight or breathability. Each has to match the mission scenario.
Third, supply at scale can be found in China today for all five capabilities. This report takes sixteen categories of the national economic industry classification, with enterprise-record counts ranging from 728 (feather and down products processing) to 57,694 (woven garment manufacturing), covering the five chains of damage tolerance, maintainability, scale-up, shelf life and environmental adaptability.
Fourth, supply is highly concentrated geographically. Across the sixteen categories, Zhejiang enters the top five sixteen times, Jiangsu fifteen times, Shandong thirteen, and Hebei and Guangdong twelve each. The reason for the concentration is the density of supporting industry: only where the material, forming, testing and certification links of a chain are all present can a complete article be made. Cost differences cannot explain this distribution; the completeness of the supporting base can.
Fifth, the five capabilities can be brought out by procurement questions. Part IV gives five sets of questions, each matched to a set of verifiable metrics and records.
The limits of this report need to be stated clearly first. All five battlefield details come from published historical material. For the multi-compartment water bucket there is only one traceable primary source, the Memoirs of Hong Xuezhi, which the paper in Dang de Wenxian follows, so this report states only that such a bucket appeared in a certain unit and does not write that it was standard equipment throughout the army. The stated volume of the fermenter differs between sources; this report keeps the "1,500 gallons" published in the media, makes no conversion, and draws no inference about output from it. Sources give two versions of when the radar battalion entered Korea, so this report states only its formation and its move to the Northeast to set up the radars, without giving a specific month. These qualifications are not gestures of modesty; they determine how far the conclusions of this report can be applied.
Part I: Questions and Scope
Chapter 1: Five Battlefield Details, Five Engineering Questions
On 25 October 1950 the Chinese People's Volunteers fought their first battle after entering Korea. For the next three years, whether equipment and supplies on the logistics lines could still be used was tested again and again by the same class of problem.
Place the five details side by side and each points to a different engineering dimension, rather than being five examples of one thing.
A bucket divided into several compartments asks whether equipment can keep working after it has been struck and damaged. Ten repaired radars ask whether something that fails can be repaired, how fast, and with what. A fermenter that will not fit asks whether what works in the laboratory can be scaled up into stable factory output. A bag of food that needs no refrigeration asks how long it keeps at room temperature and whether it spoils in transit. A winter garment that must both keep the wearer warm and let moisture out asks whether a product works normally under conditions of cold, heat, wind, water and sweat.
These five questions share one feature: none of them appears on a product's factory specification sheet. Buy a machine, a batch of material or a set of packaging, and the specification sheet will tell you dimensions, material, power rating and the standard it conforms to; it will not tell you whether the thing still works after it has been knocked, frozen, rained on or used wrongly by an operator.
This report names the five capabilities damage tolerance, maintainability, scale-up, shelf life and environmental adaptability. The names are for convenience of discussion; in engineering each has a more formal term: damage tolerance design, maintainability, scale-up, shelf life and commercial sterility, environmental adaptability. Table 1 sets out the five dimensions with their corresponding metrics.
| Capability | Question to be answered | Common metrics | Corresponding category in this report |
|---|---|---|---|
| Damage tolerance | Can it keep working after damage at a single point? | Residual strength, isolation boundary, leakage rate | Metal pressure vessels, freight containers, metal packaging containers, plastic packaging boxes and containers |
| Maintainability | How fast can it be restored after a failure? | Mean time to repair (MTTR), mean time between failures (MTBF), spare-parts fill rate | Radar and supporting equipment |
| Scale-up | Can a laboratory result be produced at stable volume? | Volumetric mass-transfer coefficient (kLa), power per unit volume, tip speed | Specialised pharmaceutical equipment, active pharmaceutical ingredients |
| Shelf life | How long does it keep at room temperature? | Water activity, F value, seal strength, leakage rate | Plastic film, specialised packaging equipment, specialised food and beverage production equipment |
| Environmental adaptability | Can it work under cold, heat, wind, water and dust? | Thermal resistance, moisture resistance, moisture-vapour transmission rate, weathering resistance | Feather and down processing, feather and down products, woven garments, knitted garments, industrial textiles, chemical-fibre weaving |
It should be noted that the relation between the categories and the capabilities discussed in this report is many-to-many. A pressure-vessel plant serves chemicals, but also food and energy; a packaging-film plant makes food packaging and industrial packaging alike. The categories are used only to locate supply, not to define capability.
Using battlefield details as the entry point is a methodological choice, not a narrative preference. Research framed by industry statistics usually starts from classification, scale and growth rate; the advantage is comparability, the disadvantage is that only the part that has already entered the statistics can be seen: how many machines or how many tonnes of material a company produced this year can be counted, while whether a machine can still supply water after being penetrated cannot. The value of the battlefield detail is that it spreads usability out over concrete objects, makes the constraints that never enter the statistics visible, and follows those constraints back to today's supply. The industrial observations obtained this way differ in dimension from a conventional scale ranking, and the conclusions therefore differ as well.
Chapter 2: Method and Data Scope
The material for this report falls into three classes.
The first class is published works and memoirs. The first issue of 2025 of Dang de Wenxian (Party Documents; issue 229 in the journal's continuous numbering) carries He Huaikai and Wei Jingyuan, "A Study of Tunnel Warfare by the Chinese People's Volunteers in the War to Resist US Aggression and Aid Korea", pp. 105–115, whose section "Support and Improvement of Tunnel Life" records the methods for storing, drawing, carrying and purifying water in the tunnels, including the multi-compartment water bucket made of thin sheet iron and scrap tyres. Section 106 of the Memoirs of Hong Xuezhi has the same passage. The construction sequence at Plant Building No. 1 of the North China Pharmaceutical Factory — large tanks installed first, walls, columns and floors built afterwards — comes from the factory's published company-history story, "Three Years to Build the Factory, Commissioned Successfully at the First Attempt".
The second class is public reporting and published historical material. The formation of Radar Battalion 101 and the repair of ten radars by CETC 14 come from the website of the State Administration of Science, Technology and Industry for National Defence, a history article from CETC 14 and public military reporting. The founding of the Shanghai Penicillin Laboratory, its floor area, its two old tanks, the successful trial production of penicillin potassium salt crystals in 1951 and the start of production in 1953 come from reports by Changning District in Shanghai and by The Paper, a biography of Tong Cun in China Pharmaceutical News, and public articles from China Science Communication and the Hongkou District Archives. The historical facts of winter clothing supply come from Xu Ping, "Winter Clothing Supply in the War to Resist US Aggression and Aid Korea", China National Defence News, 10 January 2025; the specific quantities of uniforms and bedding rushed out in July 1950 come from Xu Ping, "Cotton-padded Clothes, Cotton-padded Clothes! Why Did the CPV Not Have Any at the Chosin Reservoir?", published in the PLA Daily in 2021. The field-ration section comes from public reporting by China Military Online, the Ministry of National Defence website and CCTV.
The third class is the institute's own enterprise records. The company counts for the sixteen industry categories are counted by the middle class and small class of the national economic industry classification and include only companies whose operating status is normal, excluding companies the platform has added from other sources. The counts are numbers of enterprise records, not industry output value, not output volume and not production capacity. A single company may belong to several categories at once, so the figures for individual categories cannot be added together to represent total manufacturing output. The data were extracted in October 2026.
Enterprise-record counts and industry size are two different quantities. The records can capture how many business-scope items a company has registered and what its main products are; they cannot capture how much it makes in a year or how much it sells for, and no estimate should be derived from the records. This report therefore uses the counts only to answer "where the supply is and how dense it is", never to answer "how much capacity and how much output value". Wherever the latter questions need answering, statistical yearbooks, industry associations or company financial reports have to be consulted; this report does not substitute for them.
Several evidential boundaries need to be stated first; this is where the reader's cross-checking will begin.
First, the statement that "four fermenters were too tall for the old plant building, so the workers dug down into the ground" appears in Shanghai media reports, but could not be corroborated in factory histories, local gazetteers, memoirs or research literature, and this report does not adopt it. This report uses three verifiable facts instead: the fermenters at the Shanghai Penicillin Laboratory were rebuilt from two old tanks; Ma Yucheng improvised with large wooden vats lined with thin stainless-steel sheet; and Plant Building No. 1 of the North China Pharmaceutical Factory was built with the large tanks installed first and the walls, columns and floors afterwards. The three facts point to one question: when equipment and plant do not match, which end is changed first.
Second, sources give two versions of when the radar battalion entered Korea, 1950 and the winter of 1951. This report states only that it was formed in 1950 and that in August of that year it went to the Northeast to set up its radars, and does not give the specific month of entry into Korea.
Third, the figure for frostbite casualties at the Chosin Reservoir appears only once, in Chapter 7, to illustrate the consequences of the winter clothing supply. This report does not set out the course of the fighting and does not assess the command of the campaign.
The sixteen categories were selected as follows. For each of the five capabilities, the "manufacturing activity that carries this capability" was derived first, and the corresponding middle class or small class was then found in the national economic industry classification. Damage tolerance corresponds to the three manufacturing activities of pressure-bearing, transport and packaging; maintainability to radar and supporting equipment; scale-up to specialised pharmaceutical equipment and active pharmaceutical ingredients; shelf life to film, packaging equipment and food and beverage equipment; environmental adaptability to down, chemical-fibre weaving, industrial textiles and garment manufacturing. The selection criterion was that the activity can be clearly located in today's industry, not that it once appeared in history. This also means that Table 2 is not a complete list, only the part that this report can locate reliably using public classification and its own records.
Fourth, this report does not give the model designations, output, capacity or shoot-down numbers of equipment in current service, does not list military suppliers, and does not link companies' current products to combat uses. Wherever today's industry is involved, only public industry categories, enterprise records and product types are used.
Fifth, the engineering principles involved in the report, including compartmentalisation and isolation, maintainability, fermentation scale-up, water activity and sterilisation, thermal resistance and moisture resistance, are public engineering common knowledge; this report describes them qualitatively and does not give specific process parameters unsupported by a source. Standard numbers and standard titles follow the current published standards; test conditions may differ between versions, and in procurement the version agreed in the contract should govern.
Part II: The Engineering Mechanisms of Five Capabilities
Chapter 3: Damage Tolerance — One Compartment of Water Punctured
In the autumn of 1951 the Chinese People's Volunteers (CPV) moved their defensive works from the surface underground. The tunnels were mostly cut into the hillside, with no water source nearby: water had to be fetched from the foot of the hill and carried up, and it could not be carried in daylight, so the round trip was made at night in the intervals between shelling. The water was carried back in a sheet-metal bucket, and if a shell fragment punched a hole in it on the way, the water drained out within minutes.
A bucket then appeared at the front: thin sheet metal for the body, scrap motor-vehicle tyres for the hoops, the handle and the wear-resistant edging, and the interior divided into several compartments. If one part was hit, only the water in that compartment was lost.
The detail is recorded in He Huaikai and Wei Jingyuan, "Research on Tunnel Warfare by the Chinese People's Volunteers in the War to Resist US Aggression and Aid Korea", Party Literature, first issue of 2025. Section 106 of the Memoirs of Hong Xuezhi gives a direct account: because fetching and delivering water meant crossing mountains and running the gauntlet of fire, the soldiers made a special multi-compartment water bucket from thin sheet metal and scrap tyres, dividing the bucket into several compartments, so that once one part was hit only the water in that compartment was lost and not all of it. The same passage appears in both places; the original source that can be checked publicly is the memoir, and the paper follows it.
Take the bucket apart and it does three things.
The first is to cut one large volume into several small ones. An undivided bucket is a single continuous body of water, and a puncture anywhere drains all of it from that point; once divided into compartments, each compartment is an independent body of water, a fragment usually pierces only one point, and only one compartment is lost.
The second is to give each compartment a definite boundary. The boundary can be a partition, a folded seam, or a division formed by welding or lock seaming. The boundary does not stop fragments; what it does is confine damage that has already occurred to the place where it occurred.
The third is that the bucket could be made on the spot at the front, where manufacturing conditions were extremely poor. Thin sheet metal can be cut, folded, lock-seamed and soldered; scrap tyres can be cut into strips for hoops and handles. Neither material had to be brought up from the rear: any squad with sheet metal, tyres and simple tools could copy one. Dimensions could vary, the number of compartments could vary, the shape could vary, but the structure of compartmentalisation stayed the same. Being reproducible meant it could spread through the units, and being simple meant it could still be repaired when it broke.
Together the three make a classic design case under constraint: limited materials, limited tools, limited time, and the user is also the maker. The design goal changes accordingly. It does not aim at being unpierceable — that was impossible; it aims at controlled loss once pierced.
In engineering this line of thinking has a standard name: damage tolerance design. Its core is to accept first that damage will occur, and then to arrange the consequences after it occurs; raising absolute strength is another route. The difference between the two routes lies in their attitude to "damage": one tries to keep it from happening, the other assumes it has already happened and then works out the consequences.
In modern industry the same logic is commonly implemented by three means.
The first is compartmentalisation, cutting one large space into small spaces that do not connect. The watertight bulkhead of a ship is the earliest and most mature example: when the bottom strikes a reef, the breach opens into one compartment only, the remaining compartments still provide buoyancy, and the ship does not sink from a single hole. Multi-chamber packaging is another use of the same idea: a tube of ointment, a sachet of medical adhesive, a two-component adhesive, with mutually incompatible components packed into separate chambers and only brought together before use. Its primary purpose is to keep components that cannot be mixed from touching during storage; the isolation it produces is a side benefit.
The second is isolation: compartmentalisation separates things in space, isolation breaks the path. Check valves, shut-off valves and rupture discs on pipelines, fuses and isolating switches in circuits, module isolation and thermal-runaway isolation in traction battery packs all belong to this class. The key to isolation is that the boundary must be reliable: it must break when it should, and must not break falsely when it should not.
On pressure vessels and tank containers, isolation appears more often in the form of safety accessories. A safety valve opens and relieves on overpressure; a rupture disc bursts first at the set pressure, preserving the main body by a one-off failure; an emergency shut-off valve closes when a pipeline leaks or is struck by external force, stopping the medium from flowing out further. These accessories are not part of the pressure-retaining body, are inconspicuous in normal operation, and determine the size of the consequences under accident conditions. Their selection, set pressure, relief capacity and inspection interval are part of damage tolerance design.
The third is sealing, making the boundary inspectable and sealable. Welds on pressure vessels must be inspected for defects, valves on tank containers must be pressure-tested, seals on food packaging must be leak-tested. The difficulty of sealing is not in closing the gap but in knowing whether it has been closed: a minute leak invisible to the eye may not be measurable in the laboratory, and shows itself only after temperature changes and pressure fluctuations in transit.
Inspection of a pressure vessel usually passes through several gates: verification of materials, confirming the grade and properties of the steel plate and welding consumables; visual inspection of welds, looking for undercut, porosity and cracks; non-destructive testing by radiography, ultrasonics, magnetic particle or dye penetrant to find internal defects; a pressure test, pressurising with water or gas to the specified value, looking for deformation and leakage; and a tightness test, using soap solution, helium leak detection or pressure decay to find minute leaks. Each gate has a standard, a record and a responsible person.
All three means have costs. Compartmentalisation loses effective volume and adds structural weight and manufacturing steps; isolation adds valves, sensors and control logic, and adds failure points; sealing raises machining precision and inspection cost. A multi-compartment water bucket is heavier, more laborious to make and holds less water than a single-compartment bucket of the same volume. The battlefield accepted that cost because the rate at which water arrived mattered more than the capacity of the bucket.
It should be noted that damage tolerance only limits the consequences of a single breach; it does not eliminate damage. It must be paired with inspection, spares and repair procedures. A pressure vessel that has been compartmentalised but is not periodically inspected, with a partition corroding unnoticed, is compartmentalised in name only; a multi-chamber package whose seals are not strong enough, so that the chambers communicate, loses the point of being divided.
One further cost of damage tolerance design is easily overlooked: it increases the complexity of the system. One more partition, one more weld, one more valve is one more place where something can go wrong. Compartmentalisation breaks one large risk into several small ones while increasing the number of small risks. What engineering has to calculate is whether the total risk really falls after the split, not merely how any single compartment performs.
Chapter 4: Maintainability — Ten Radars Restored
On 22 April 1950 the Central Military Commission ordered the formation of an Air Force signals battalion. The unit was later renamed Radar Battalion 101 of the Chinese People's Liberation Army, the first radar battalion of the Chinese armed forces; in August of the same year it moved to the Northeast and set up radars along the border.
Where did the equipment come from? China had no radar industry at the time; what old China left behind was a few repair and fitting shops, several batches of captured equipment and a scattered body of technicians. The only organisation capable of restoring radars systematically was one: the Radar Research Institute in Nanjing, the predecessor of today's CETC 14. It had no complete drawings, no complete spares and no production line, only damaged Japanese and American radars captured in the war, and a group of technicians who understood vacuum tubes, antennas and receivers.
The institute's own history records that, under conditions of extreme material scarcity, it restored a first batch of radars, ten in all. Those ten radars were the entire equipment of the first radar battalion; the institute also sent technicians to move with the equipment.
Ten is a very small number, but it draws a line: when a country cannot yet build a certain kind of equipment, it must at least be able to repair it. Repair is the first step of industrial capability, manufacture the second, and between the two lies a whole chain of materials, processes, components, testing and standards.
Repairing a captured radar is quite different from changing a circuit board at a repair shop today. First, the models were mixed: Japanese and American, from different makers, different years and different systems, each with possibly different circuit architecture, component specifications and connector types, so each set had to be understood before it could be repaired. Second, parts were missing: captured equipment was often incomplete, lacking power supplies, antennas, displays, even drawings, and with no spares the only option was to take parts from a scrapped set of the same model. Taking a part was not a matter of fitting whatever happened to match: the operating point had to be recalculated, gain, bandwidth and frequency stability remeasured, and the performance of the whole set confirmed not to have drifted after the swap. Third, instruments were scarce: repairing radar requires signal sources, oscilloscopes, frequency counters and power meters, all scarce at the time, so technicians had to judge whether a module was good or bad with the few instruments on hand, plus measurement and experience. Fourth, what had to be restored was performance, not power: lighting up is not detection, and whether transmit power was sufficient, receiver sensitivity adequate, the antenna pattern correct and ranging accuracy within tolerance all had to be verified on site, against real targets. Fifth, the users had to be taught: the technicians moved with the equipment, and did not merely repair but installed, sited, adjusted and trained the operators.
Only these five things together are the full meaning of "repair": to find the location of failure, to restore specified performance, and to let the user keep it going in the field.
Translated into engineering language, this history is maintainability. Maintainability is not the phrase "easy to repair"; it can be broken down into five conditions.
The first condition is accessibility. When a failure occurs, can a person reach it? Whether the cabinet door opens easily, whether a module sits within reach or three parts must first be removed, whether piping and harnesses block the inspection opening. In equipment with poor accessibility, most of the repair time goes into dismantling and reassembly, not into finding the fault. Accessibility also includes mistake-proofing: plugs must not go in the wrong way, modules must not fit the wrong slot, pipes must not connect to the wrong port. Where mistake-proofing is well done, repair does not depend on an old hand's memory; where it is poorly done, one wrong insertion can enlarge the fault.
The second condition is modularity. Can a whole block be replaced? The equipment is divided into a number of line-replaceable units (LRUs), and the field does only "judge, replace, verify", leaving soldering and adjustment to the rear. The higher the degree of modularity, the faster the field repair, and the greater the demand on spare-parts supply.
The third condition is testability. Can the fault be located? The equipment needs test points, built-in test (BIT) routines and the ability to isolate a fault to a given unit. Without testability, repair is guesswork; with guesswork, good units come out and bad ones stay in.
The fourth condition is spares. Is there something to replace with? Critical parts, wearing parts and consumables need reasonable stocks. The variety and quantity of spares set the ceiling of repair capability; the supply lead time of spares sets the floor of downtime.
The fifth condition is people, and documentation. Is there someone who can repair, and something to consult? Maintenance manuals, circuit diagrams, wiring diagrams, fault trees and training records look like paperwork but in practice determine whether repair capability can be reproduced. That one old hand can repair does not mean a unit can repair; only when experience is written into documents and taught to a group of people does the capability remain.
These five conditions correspond in engineering to a group of metrics: mean time to repair (MTTR), mean time between failures (MTBF), the line-replaceable unit (LRU), built-in test (BIT) and spare-parts fill rate. The names may differ; the question they point at is the same: once the equipment fails, how quickly can it be restored, and by what means.
Repair is not one person's business; it is a tiered system. Organisational-level maintenance is performed at the operating site: the operator does daily checks, cleaning, tightening, and replacement of fuses and exposed modules, with the aim of restoring basic function without waiting for someone from the rear. Intermediate-level maintenance is performed at brigade or regimental repair shops or bases, with test equipment, a spares store and a repair bench, and can do board-level or assembly-level replacement and isolate a fault to a line-replaceable unit. Depot-level maintenance is performed at a factory or research institute, doing deep repair, component-level replacement, performance calibration, overhaul and software upgrades.
The three levels are connected by spares and transport. Spares fall into several classes: consumables, used up once and gone, such as fuses and sealing rings; wearing parts, short-lived and requiring periodic replacement; repairable items, which can be repaired and returned to store; non-repairable items, which can only be scrapped when they fail; and rotable items, costly and few in number, replaced first and repaired later. The variety and quantity of spares determine what each level of repair can do, and the transport lead time for spares determines how long equipment stays down.
This system takes a different form in the vacuum-tube era and in the solid-state era. Vacuum tubes are bulky, run hot and have short lives, but they can be pulled out and replaced. When a radio set failed, the operator opened the cabinet, saw which tube was not glowing, pulled it out and put in another, and the set recovered; testing was direct too, measuring voltages with a multimeter, looking at waveforms on an oscilloscope and injecting a signal with a signal source. The maintainability of tube equipment rested on parts being large, reachable and replaceable.
In today's equipment the chips are mounted on the board, in ball-grid-array packages, with the pins underneath the chip, out of reach in the field. When it fails, the whole board is replaced, or the whole set goes back to the factory. Maintainability has moved from repairing parts to swapping modules, from repair in the field to tiered exchange. This speeds repair, and also increases dependence on spare-parts supply and module standardisation: the faster modules are exchanged, the greater the pressure on the spares store; the more expensive the spares, the higher the cost of downtime.
Maintainability has its costs too. Modularity adds connectors, and connectors bring contact resistance and new failure points; testability adds sensors and circuits, and adds cost; spares stocks tie up capital and warehousing; maintenance documentation adds design and training workload. Maintainability must therefore match the mission scenario, and there is a right degree of it: equipment installed on a remote mountain top, where a repair trip takes hours of driving, must have far higher maintainability requirements than equipment standing in a workshop.
Repair has a further limit: cannibalisation reduces the number of usable sets. Taking parts from a set of the same model in an emergency to restore one set often leaves another standing idle; the more is taken, the fewer sets can be powered up. However strong the repair capability, it cannot hold out for long without new equipment to replenish it. This is also why being able to repair is only the first step — to go further, a country must have materials, components, processes, testing and standards, and be able to design and manufacture for itself.
Chapter 5: Scale-up — A Fermenter That Would Not Fit
In March 1950, with the approval of Mayor Chen Yi, the Shanghai Penicillin Laboratory was established, headed by the microbiologist Tong Cun. At its founding it had twelve people, eight of them technical staff; a plant area of 2,510 square metres; and as its main equipment a fermenter rebuilt from two old tanks. The laboratory designed, machined and installed the entire penicillin production equipment itself.
In April 1951 the laboratory succeeded in producing penicillin potassium salt crystals on trial, the first penicillin made in China. Production began formally on 1 May 1953; in the same year the laboratory was renamed the State-Operated Shanghai No. 3 Pharmaceutical Factory, under the Pharmaceutical Industry Administration of the Ministry of Light Industry. The first batch of domestically made penicillin was produced in a 1,500-gallon fermenter.
The difficulty at the time was not only that the equipment was small. Stainless-steel fermenters could not be bought, and Ma Yucheng, who was transferred to Shanghai in 1952 to help found the factory, thought of a way: he asked for a wooden vat large enough, lined it with thin stainless-steel sheet, and used that as a stopgap. The wooden vat could hold liquid, the stainless sheet could contact the medium, and together they made a serviceable fermenter.
The workaround makes one point: at a stage when the industrial base is weak, equipment can be substituted, but the process cannot. Fermentation needs sterility, aeration, agitation and temperature control; without any one of them the culture grows poorly, or the whole batch is contaminated and lost. What was substituted was the vessel; sterility, aeration, agitation and temperature control could not be dropped.
The North China Pharmaceutical Factory took another route. The factory began preparations in 1953 as one of the pharmaceutical projects in the "156 Projects", broke ground in 1955 and went into production in 1958. Building No. 1 of the antibiotic plant was to house 32 fifty-cubic-metre fermentation tanks for penicillin and streptomycin. The equipment came from the Soviet Union in several shipments, and delivery was repeatedly delayed; civil works waited for equipment and equipment waited for civil works, with the schedules compressed together. The joint command eventually decided: install the big tanks first, and build walls, columns and floor slabs afterwards — first complete the ground-floor foundation, lift the big tanks into position, and then build walls, erect columns and pour slabs around them.
Such a sequence is uncommon in factory construction today. The conventional practice is to build the building and then bring in the equipment; if the equipment will not go in, a hole is left in the wall, or the roof is left to the end. The North China Pharmaceutical Factory went further: the building grew around the equipment.
The two answers point in opposite directions and share one logic: the equipment is the core, the building is the shell. When the equipment outgrows the building, or the arrival of equipment disrupts the construction sequence, it is the shell that changes, not the core.
The real difficulty lies in scale-up itself. Industrial production of penicillin uses submerged fermentation: the producing organism is placed in a huge tank filled with culture medium, sterile air is sparged in, the contents are agitated and temperature-controlled, and the organism grows in the liquid, metabolises and secretes penicillin. After fermentation the cells are filtered out, penicillin is extracted from the filtrate, then crystallised and dried into the active pharmaceutical ingredient. In the laboratory this step can be done in a shake flask on a shaker, where shaking brings the liquid surface into contact with air; in the production tank the volume goes from a few hundred millilitres to tens of cubic metres, a hundred-thousandfold increase. Scale-up is not enlarging a shake flask proportionally.
The first problem is oxygen. The producing organism is aerobic; oxygen dissolves poorly in water, and the oxygen in the medium is carried in by air bubbles, with agitation breaking the bubbles up and turning the liquid over. The measure of oxygen supply is the volumetric mass-transfer coefficient (kLa) — in plain terms, how much oxygen passes from the bubbles into the liquid per unit time. The larger the tank, the more the residence time of the bubbles, their distribution and the flow field produced by agitation change. An aeration rate adequate in a small tank may be insufficient in a large one; raising it brings foaming, shear and energy consumption in turn.
The second problem is heat. Metabolism of the organism produces heat, and agitation produces heat too. A small tank is adequately cooled by a jacket; a large tank has a small surface-area-to-volume ratio, can dissipate less heat per unit volume, and cooling capacity easily becomes the bottleneck. The problem is more pronounced in summer, in hot regions and in high-density culture.
The third problem is mixing. The flow field generated by the impellers in a large tank cannot be uniform everywhere: near the impeller shear is strong and dissolved oxygen high, while far from it dead zones may form. Organisms in a dead zone lack oxygen and nutrients, change their metabolic direction and produce less. Scale-up must consider impeller type, number of stages, diameter and speed, as well as the baffles and draft tube in the tank.
The fourth problem is sterility. Once fermentation is contaminated, the contaminants compete with the producing organism for nutrients and produce proteases that break down the product, and the whole batch is lost. A large tank has many welds, and valves, flanges, mechanical seals, sampling ports and feed ports are all potential leak points; the medium must be thoroughly sterilised, the air filtered, and the equipment capable of sterilisation in place. One aged gasket can waste tens of tonnes of medium.
To push contamination risk down, the plant does three things: cleaning, circulating alkaline solution, acid solution and hot water through the tank to wash out residual medium and cells; sterilisation, heating the tank, piping and valves with steam to a specified temperature and holding it long enough; and validation, using temperature records, indicators and microbiological challenge tests to prove that cleaning and sterilisation are actually effective. Cleaning, sterilisation and validation together are what sterile production means.
The fifth problem is control. Sugar, nitrogen and precursors must be fed; temperature, pH and dissolved oxygen controlled; and the process adjusted according to the morphology of the organism and its metabolic curve. Fed-batch culture means feeding while fermenting, keeping the cell concentration and the accumulation of product in a suitable range. How much to feed, when to feed, and at what concentration and rate must all be worked out afresh during scale-up.
The sixth problem is downstream. The penicillin concentration in the broth is low, and the broth carries cells, proteins, pigments and organic acids; it must go through filtration or centrifugation, solvent extraction, crystallisation, washing and drying. Every step loses yield, and every step has its own scale-up problems.
These six problems together are the real meaning of the word "scale-up". The laboratory settles whether it can be made at all; the factory settles whether it can be made every day, in every batch, consistently. Between the two lies a whole body of process knowledge, of which a production line is only the visible part.
Scale-up is not only a matter of what happens in the tank; the strain and the medium are variables too. Fermentation starts with the strain, and after decades of breeding the producing organism yields orders of magnitude more than the original isolate; breeding relies on mutation, screening and rescreening, generation after generation, to pick strains of high yield, few impurities and genetic stability; strains must be preserved, rejuvenated and protected against degeneration. Beyond the strain is the medium, which must supply carbon, nitrogen, inorganic salts and trace elements, and also the precursors for synthesis. Lactose was used as the carbon source in the early years, later glucose; nitrogen sources are commonly corn steep liquor, soybean meal and cottonseed meal; precursors steer side-chain synthesis. The formulation is not fixed; it must be adjusted to the strain, the tank, the process and the batch of raw material.
Three criteria are commonly used in engineering to guide scale-up: constant volumetric mass-transfer coefficient, constant power per unit volume, and constant tip speed. The first preserves oxygen supply, the second preserves agitation intensity, the third preserves shear conditions. The three criteria often cannot be met at once: scaling on constant mass transfer may leave agitation power insufficient; scaling on constant power per unit volume may make tip speed too high and damage the organism. Scale-up is the search for a balance among conditions that cannot all be satisfied at the same time.
Scale-up is not free. The larger the tank, the lower the fixed cost per unit of product; but the loss from one contaminated batch is also larger, the energy for cooling, aeration and agitation higher, the time for cleaning, sterilisation and validation longer, and the load on downstream filtration, extraction and crystallisation heavier. Benefits and risks scale up together.
A fifty-cubic-metre fermenter contaminated once loses fifty cubic metres of medium, the corresponding raw materials, energy, labour and production schedule; a five-hundred-litre pilot tank contaminated once loses far less, and the cause is easier to trace. This is why plants usually keep a pilot line: it may not make money, but its job is to expose problems before scale-up.
Scale-up must also look downstream. Fermentation is only the first step; if extraction, crystallisation and drying cannot keep up, the product of fermentation piles up in the middle and becomes a bottleneck. In many plants capacity expansion is held back by downstream separation and purification, and fermentation is not the bottleneck at all.
So the optimal scale for scale-up is not the largest possible. It must match market demand, raw-material supply, utilities, environmental capacity, the quality system and financial strength. Scale is the means; stable supply is the purpose.
Chapter 6: Shelf Life — How Long a Bag of Food Keeps
In the winter of 1950, in the valleys of the northern Korean peninsula, CPV soldiers carried a field ration in their pockets: roasted wheat flour (chaomian). Wheat flour was roasted, salt added, and in some places soybean flour, corn flour or sorghum flour mixed in; it was packed into cloth bags and carried on the person. To eat, one took a handful, put it in the mouth and swallowed it with a mouthful of snow. No heating, no bowl or chopsticks, no refrigeration, and it did not spoil for a while.
The front chose it for direct reasons: it could be made in large quantities, stored for a long time, carried on the back, and eaten while fighting. All four conditions were indispensable. Hot food was of course better, but hot food required a cookhouse, stoves, fuel and time, and a relatively safe rear area; under shelling interdiction, with units dispersed and constantly moving, the radius within which hot food could be guaranteed was very short. Roasted wheat flour moved cooking off the battlefield to the rear, and compressed eating into taking a handful from a pocket.
That roasted wheat flour kept, it owed to two things: dry, and cooked. Roasting brought the moisture in the flour down to a very low level, and without water microorganisms cannot grow; the roasting temperature also killed most microorganisms and insect eggs.
Roasted wheat flour had obvious shortcomings: too dry to swallow easily; nutritionally unbalanced, mostly carbohydrate, short of fat, protein and vitamins; eaten alone over the long term, it sapped strength and resistance. These shortcomings were hard to solve under the industrial conditions of the time; solving them depended on the food industry that came later: cans, compressed rations, flexible packaging, self-heating foods.
The scale of supply also shows its place indirectly. According to Xu Ping's research, the Volunteers needed 14.82 million jin of roasted wheat flour a month, and the Northeast alone could supply only 10 million jin; from entry into Korea to June 1951, more than 30,000 tonnes of this kind of field ration were shipped forward. A single frontline ration item required production and transport across several greater administrative regions; that is itself a question of industrial organisation.
Whether a food can be stored at ambient temperature turns on one core measure: water activity. Water activity is not moisture content: moisture content is how much water there is, water activity is how much of that water microorganisms can use. Foods with the same moisture content differ in water activity after sugar or salt is added, or after drying or freezing, and microorganisms may or may not grow. Most bacteria stop growing below a water activity of 0.9; moulds and yeasts tolerate lower values. Bring water activity below the tolerance line of microorganisms and the food can be kept at ambient temperature.
The other route is sterilisation. The food is packed into a sealed container, heated to a sufficiently high temperature to kill the microorganisms inside, and kept sealed so that outside microorganisms cannot get in; the food then keeps for a long time. Canning follows this idea. The measure of sterilisation intensity is the F value, which converts a combination of sterilisation temperature and time into one equivalent value. Low-acid foods generally have to be sterilised at around 121°C to kill the spores of Clostridium botulinum.
The retort pouch is a variant of the can. It replaces the rigid container with a flexible laminated film bag: an outer printing and strength layer, a middle barrier layer, an inner heat-seal layer. The food is filled, vacuumised or nitrogen-flushed, heat-sealed, and then heated in a retort to sterilise. Compared with glass jars and tinplate cans, the retort pouch is lighter, thinner, takes up less space, heats through faster, and is eaten straight from the bag, which suits carrying.
The retort pouch is not a new invention. In the late 1950s the US Army Natick Laboratories began developing retort pouches to replace tinplate cans for military food, later working with can-making companies to produce a three-layer pouch of polyester, aluminium foil and polyolefin; in 1969 such foods were used in the Apollo programme. The military needed food lighter than cans, better tasting than compressed rations and openable under field conditions; spaceflight needed packaging that allowed eating in weightlessness and produced no crumbs; the retort pouch met both requirements at once, later entered the civilian market, and became today's retort-packed braised foods, ready meals and wet pet food.
Self-heating food goes half a step further. It does not solve storage; it solves how to make a meal hot when there is no hot water. The typical construction has three layers: the food bag, the heating pad and the outer bag. The heating pad releases heat on contact with water, and the steam heats the food; the food itself is still pre-cooked, sealed and storable at ambient temperature. The heating pad only moves the last step of heating from the cookhouse to the soldier's hands.
There are two common types of heating pad. One is based on quicklime, which forms slaked lime and releases heat on contact with water; the material is cheap and the reaction mild, but the heat released per unit weight is limited and heating takes longer. The other is based on magnesium alloy, which reacts with water and releases heat; heat output is high and the temperature rises fast, but the reaction gives off hydrogen, so venting and ventilation must be considered in packaging and use. Which one to choose depends on the weight of the food, the ambient temperature, the time available and the safety requirements.
Aseptic packaging is another technical route. It sterilises food and packaging separately: the food by ultra-high-temperature flash sterilisation, the packaging material by chemical or irradiation means, followed by filling and sealing in an aseptic environment. Aseptic packaging suits heat-sensitive foods such as milk and juice and retains flavour and nutrients better. The difference from the retort pouch is that the retort pouch fills first and sterilises afterwards, while aseptic packaging sterilises first and fills afterwards.
A bag of food that keeps for months at ambient temperature rests on a system, not on a single packaging film. The system has five layers.
The first layer is barrier. When food spoils, the problem often lies with oxygen, moisture vapour and light, and microorganisms are only part of the cause. Fats oxidise and turn rancid, vitamins degrade, pigments fade. Common barrier layers are aluminium foil, ethylene-vinyl alcohol copolymer, and films coated with aluminium oxide or silicon oxide. Aluminium foil has the best barrier but is opaque and cannot go in a microwave; coated films are transparent and microwaveable, but their barrier depends on the integrity of the coating. Multilayer laminates combine the strengths of different materials: an outer layer for wear and printing, a middle layer for barrier, an inner layer for heat sealing.
The second layer is the seal. The seal of a flexible package is a heat-sealed seam, where temperature, pressure and time fuse the two inner layers. A seal that is too weak opens in transit; a seal that is too strong cannot be torn open by the consumer; residues caught in the seal area form channels through which microorganisms and oxygen enter. Seal width, the temperature curve and pressure uniformity must all be controlled in equipment and process.
The third layer is sterilisation. Retort pouches go into a retort and are heated with hot water or steam. The temperature distribution inside the retort must be uniform, or some pouches are under-sterilised and others overheated. Flexible packages expand when heated, so counter-pressure must be applied in the retort to prevent bursting. The centre temperature of the product must reach the set value and be held long enough, and sterilisation records must be traceable, because they are the key evidence for food safety.
The fourth layer is testing. Seal strength is measured, leaks are detected, tightness is verified; common leak-testing methods are dye penetration, vacuum decay, pressure decay and laser headspace analysis. Shelf life must be verified by accelerated testing: samples are held at high temperature and high humidity, and microbiological, sensory and physicochemical indicators are measured periodically to extrapolate the shelf life at ambient temperature.
The design of an accelerated test has to fix several parameters: the test temperatures, commonly set as gradients of 30, 40 and 50 degrees Celsius; the test humidity, determined by the water activity of the product and the barrier of the package; the testing intervals, converted according to the temperature gradient; and the indicators measured, including microbiological, sensory, physicochemical and package integrity. For every 10 degrees Celsius rise in temperature, the rate of chemical reaction roughly doubles, and this rule of thumb can be used for extrapolation; but microbial growth and the ageing of packaging materials do not necessarily follow the same rule, so the conclusions of accelerated testing must be verified against samples held at ambient temperature. Accelerated testing shortens the wait; it cannot replace verification in real time. Transport packaging must also undergo drop, stacking, vibration and puncture tests to confirm that it will not be damaged in the logistics chain.
The fifth layer is matching material to contents. Acidic foods may corrode aluminium foil, oily foods may permeate the inner layer, foods containing alcohol may change the swelling behaviour of the inner layer, and high-temperature sterilisation may cause some materials to leach. Suppliers must know the pH, fat content, water activity and sterilisation conditions of the contents in order to choose the right structure.
Only these five layers together are the packaging industry behind a bag of food. Putting food into a bag is only the surface; behind it is a chain linking materials, sealing, sterilisation, testing and transport. If any link in the chain fails, the shelf life shortens or safety gives way.
A longer shelf life is not automatically better. Extending it exacts a price in three respects: flavour and nutrition — the higher the sterilisation temperature and the longer the time, the greater the loss of flavour compounds and vitamins; packaging cost — the thicker the barrier and the more layers, the higher the material cost and the harder the recycling, since aluminium-foil laminates are hard to recycle while recyclable mono-material packaging has poorer barrier than a laminate; and energy — the retort must be heated, held and cooled, aseptic filling must maintain a clean environment, and the cold chain must refrigerate throughout. Shelf life must be matched to the consumption scenario: fresh milk drunk locally within three days does not need a six-month shelf life, while self-heating rice sent to remote areas needs a longer shelf life and stronger packaging. A shelf life that is too long is waste; one that is too short is risk.
Chapter 7: Environmental Adaptability — Two Contradictions in a Winter Garment
In October 1950 the CPV entered Korea. Units were assembled from the south, from the central plains and from the Northeast and moved into the northern part of the Korean peninsula, and the problem of clothing and equipment was quickly exposed.
On 10 January 2025 Xu Ping published "Winter Clothing Support in the War to Resist US Aggression and Aid Korea" in China National Defence News, reviewing the clothing and equipment support of the time. The quantities rushed out come from his article "Cotton Padded Clothes, Cotton Padded Clothes! Why Did the Volunteers Not Have Them at the Battle of Chosin Reservoir?", published in PLA Daily in 2021: from July 1950 the General Logistics Department arranged for the Northeast, North China, East China and Central-South military regions to rush out 340,000 padded suits, 360,000 pairs of padded leather shoes, and 400,000 each of padded caps, fleece trousers, padded vests and padded overcoats; and 700,000 pairs each of padded gloves and socks. The numbers look substantial, but the units entered Korea faster still, and the transport lines were bombed, so much of the material did not reach the front before the severe cold.
The case of the 9th Army Corps was the most typical. The corps had been on standby in the south, and when it was rushed into Korea it had only the thin cotton jackets issued for the south. Night temperatures in the Chosin Reservoir area fell to minus 40 degrees Celsius. On its first day of marching the 27th Army had more than 700 cases of frostbite.
In 1951 the logistics departments improved their transport methods. Summer clothing lost 30 per cent to the "strangulation campaign"; winter clothing, 1.43 million sets, was carried by the "one-sided continuous running" method and the loss fell to 0.52 per cent, and the units were in padded jackets a month before their opponent. In the same year Zhou Enlai directed that the Volunteers' uniforms must use new cotton. New cotton insulates better than old, and the requirement was a direct response to the frostbite reported from the front.
On 22 June 1951 the General Logistics Department issued the "Directive on the Style and Quality of Winter Uniforms for the Chinese People's Volunteers", stipulating that each padded suit be filled with four and a half jin of cotton, with cadres and soldiers on the same standard. At the time, PLA padded jackets in the north generally used four jin, in the south two to two and a half jin, and in some cases under two jin. The figure of four and a half jin was the result of converting the use scenario of "operations in a cold region" directly into a material quota — the standard was not set out of thin air but inferred backwards from the operating environment.
At the Battle of Chosin Reservoir the 9th Army Corps lost 28,954 men to frostbite and 19,002 in battle casualties. The figures say one thing: under extreme cold, the insulating capacity of a garment bears directly on the fighting strength of a unit.
Clothing does not generate heat; it, together with the layer of air beneath it, slows the transfer of body heat outwards. Still air is a good insulator, and the function of cotton, down and hollow fibre is alike: to hold air still, forming layer upon layer of minute pockets of still air.
Cotton fibre absorbs moisture. When a person sweats, the cotton takes up the water, the fibre swells, the air layer is compressed and insulation falls; evaporation of the water then carries heat away, making the wearer feel colder. A soaked cotton jacket is heavy and dries slowly. In a dry, still environment cotton is reliable; in a damp, active one its shortcomings are obvious.
Down has the highest insulating efficiency. A down cluster has a three-dimensional structure that holds a large amount of air, and its insulating capacity for the same weight is far above cotton. Two measures are commonly used for down: down content, the proportion of down clusters in the down and feather, called "down percentage" in the old standard; and fill power, the volume occupied by a given weight of down under a given pressure. The higher the fill power, the stronger the ability to hold air. The weakness of down is that it fears moisture: once damp, the clusters stick together, the air layer collapses, insulation falls sharply, and in the field it is very hard to restore.
Hollow fibre is one direction within synthetic fibres. Polyester made into a hollow or porous structure can hold air both inside the fibre and between fibres. Its insulation is below that of high-fill-power down, but it retains part of its insulating capacity when damp, dries fast, costs little and washes easily. Much of today's insulated clothing mixes down and hollow fibre: down for the torso, synthetic fibre for the parts that sweat easily.
These materials solve insulation. The real difficulty is insulating while letting moisture vapour through.
The body sweats when it moves, and evaporation of sweat carries heat away. If the garment does not breathe, the vapour is trapped inside, first feeling hot and stuffy, then damp, then rapidly cold once the wearer stops; if the garment breathes too freely, the wind carries the heat away. A good winter garment must do three things at once: block the wind and liquid water outside, let water vapour inside escape, and keep a sufficiently thick still-air layer when the wearer is at rest.
A single layer of material can hardly do all three, and the usual solution is layering. The inner layer sits against the skin and its job is to move sweat: a quick-drying synthetic fabric draws sweat from the skin surface to the outer face of the fabric and enlarges the evaporation area; cotton underwear absorbs sweat but does not dry quickly, which works against the wearer in a cold environment. The middle layer insulates: fleece, down, padded garments and wool sweaters hold air, and there may be several such layers adjusted to the temperature. The outer layer protects: windproof, waterproof, abrasion-resistant, usually with a water-repellent finish and taped seams to keep rain from seeping through the stitching.
The conflict between waterproofing and breathability is eased by membrane materials. Expanded polytetrafluoroethylene membrane, commonly called PTFE membrane, has a large number of micropores whose diameter is smaller than a water droplet and larger than a water-vapour molecule, so liquid water cannot enter and water vapour can leave. A PU hydrophilic membrane has no micropores and passes water molecules along hydrophilic groups on the polymer chain; it is better at waterproofing and slightly weaker at breathability. Each has its trade-off, and products in practice are often built as composites.
Beyond materials, structural detail also determines how a garment wears: the fit of the hood, the height of the collar, the tightness of the cuffs, the drawcord at the hem, the underarm ventilation zips and the position of the pockets all affect insulation and breathability. The insulation value a garment measures in the laboratory may be quite different in wind, in snow and in motion.
A down jacket passes along a long chain from raw material to finished garment. Down begins as raw feathers, with duck down and goose down graded by origin, season and species; the raw feathers carry feather vanes, impurities, dust and grease, and must first be sorted, then washed, dewatered and dried; after drying the material is separated, dividing down clusters from feather vanes and batching by down content; then come dust removal and blending, combining batches into a stable raw material. Down is specified not only by down content but by fill power, cleanliness, oxygen consumption, residual fat and moisture content: down content determines how much down there is, fill power how much air the down can hold up, cleanliness whether there is odour and impurity.
Making the garment also requires down filling. Before filling, the down-proof baffle fabric is made: it must be down-proof, with sufficient density and moderate air permeability; a filling machine blows the down into each baffle by fill weight, and the size and shape of the baffles and the fill weight determine how insulation is distributed — too little and cold spots appear, too much and the garment is bulky and hard to move in; after filling, the openings are closed, the down patted even and the garment checked to prevent down leakage and migration. The shell fabric is another chain: synthetic filament or staple is woven into cloth, then dyed and finished, the finishing including water repellency, coating, lamination and calendering; waterproof-breathable fabrics usually bond membrane and fabric together into a two- or three-layer laminate; seams must be taped and needle holes sealed with tape.
The insulating capacity of a garment is the joint result of the down, the baffle fabric, the shell fabric, the lining, the stitching, the down filling and the construction. If any one link fails, the performance of the whole garment drops: down getting damp, baffle fabric leaking down, a shell that does not breathe, seams leaking water, uneven filling — any of these puts the wearer at a disadvantage in a cold environment.
Insulation and breathability cannot be judged by hand; they must be tested to standards. Thermal resistance measures a fabric's ability to impede heat transfer, commonly expressed in clo; moisture resistance measures its ability to impede water-vapour transfer, commonly expressed as the RET value, the lower the RET the better the breathability; moisture-vapour transmission rate is the amount of water vapour passing through a unit area of fabric in unit time. Among current textile test standards, GB/T 11048 is used to determine the thermal resistance and moisture resistance of textiles under steady-state conditions, GB/T 12704 to determine the moisture-vapour transmission of fabrics, by the desiccant method and the evaporation method; for down, GB/T 17685 sets the technical requirements for down and feathers, and GB/T 14272 is the product standard for down garments. These standards specify test conditions, specimen dimensions and calculation methods so that results from different laboratories can be compared.
Three things matter when reading a test report: the test method, which standard was used for thermal resistance, moisture resistance and moisture-vapour transmission and under what conditions; the testing body, whether it is accredited and whether the report can be traced; and the test sample, whether it is the same material and the same construction as the production goods. Between a small specimen in the laboratory and the insulation of a finished garment lie stitching, down filling, interlayer construction and the way the garment is worn.
Standards settle comparability; they do not settle applicability. A garment labelled with high-fill-power down, worn in a damp environment, may insulate less well than an ordinary synthetic padded jacket; a shell jacket labelled with a high moisture-vapour transmission rate, once its outer face is caked with mud, loses its breathability. A test report is a starting point, not an end point.
This is why the winter clothing problem of 1950 could not be solved merely by issuing more padded jackets. There had to be cotton, factories, transport, distribution, forward delivery and replacement, and also styles and constructions matched to the battlefield environment. Clothing and equipment support is a chain, and the garment is only one link in it.
Part III: Today's Industrial Supply
Chapter 8: Supply Baselines for Sixteen Industry Categories
All five capabilities can find supply at scale in China today. This report takes sixteen industry categories of the national economic industry classification as its observation window; Table 2 gives the number of enterprise records nationwide and the five leading provinces.
| Capability | Industry category | National total | Top five provinces |
|---|---|---|---|
| Damage tolerance | Metal pressure vessel manufacturing | 1,932 | Jiangsu 373, Shandong 308, Zhejiang 197, Hebei 123, Henan 118 |
| Container manufacturing | 1,132 | Guangdong 180, Hebei 158, Jiangsu 154, Shandong 128, Zhejiang 57 | |
| Metal packaging containers and materials manufacturing | 4,798 | Guangdong 772, Jiangsu 722, Shandong 585, Zhejiang 505, Hebei 485 | |
| Plastic packaging boxes and containers manufacturing | 23,625 | Guangdong 4,895, Zhejiang 3,416, Shandong 2,534, Jiangsu 2,389, Hebei 2,115 | |
| Maintainability | Radar and supporting equipment manufacturing | 845 | Jiangsu 159, Guangdong 155, Zhejiang 104, Shandong 48, Anhui 43 |
| Scale-up | Special-purpose pharmaceutical equipment manufacturing | 1,354 | Jiangsu 334, Zhejiang 303, Shanghai 155, Shandong 111, Hebei 59 |
| Chemical pharmaceutical ingredient manufacturing | 3,211 | Shandong 320, Jiangsu 311, Zhejiang 293, Anhui 209, Hubei 196 | |
| Shelf life | Plastic film manufacturing | 22,844 | Guangdong 5,972, Zhejiang 3,162, Jiangsu 2,819, Shandong 2,470, Hebei 2,047 |
| Special-purpose packaging equipment manufacturing | 2,541 | Guangdong 519, Zhejiang 490, Hebei 363, Jiangsu 333, Shandong 279 | |
| Special-purpose equipment manufacturing for food, wine, beverage and tea production | 3,240 | Shandong 647, Hebei 521, Zhejiang 444, Guangdong 357, Jiangsu 320 | |
| Environmental adaptability | Feather (down) processing | 1,125 | Henan 196, Anhui 195, Hebei 112, Zhejiang 100, Guangdong 74 |
| Feather (down) product processing | 728 | Zhejiang 279, Anhui 64, Henan 58, Jiangsu 56, Hebei 53 | |
| Chemical fibre weaving | 18,007 | Zhejiang 7,449, Jiangsu 6,332, Shandong 900, Guangdong 664, Hebei 646 | |
| Industrial textile product manufacturing | 24,720 | Zhejiang 5,650, Jiangsu 4,444, Shandong 3,280, Guangdong 3,182, Hebei 2,233 | |
| Woven garment manufacturing | 57,694 | Guangdong 13,959, Zhejiang 12,096, Jiangsu 5,903, Fujian 4,120, Anhui 3,893 | |
| Knitted or crocheted garment manufacturing | 23,731 | Zhejiang 8,022, Guangdong 5,229, Jiangsu 2,212, Shandong 1,962, Fujian 1,320 |
Source: the Institute's enterprise records. Counted by middle class and small class of the national economic industry classification, covering only enterprises operating normally and excluding companies the platform has added from other sources. The counts are enterprise records, not output value, output volume or production capacity. The same enterprise may belong to several categories at once, so the figures in different rows cannot be added together; this report therefore gives no total. Data extracted in October 2026.
Three points need attention when reading this table.
First, the absolute sizes of the figures differ greatly. The smallest category is feather-down product processing, with 728; the largest is woven garment manufacturing, with 57,694. The two figures differ by a factor of nearly eighty, but whether the chain behind each of them is complete or broken cannot be read directly from the number of enterprises. Enterprise counts answer where, not whether it is any good.
Second, a single capability is often carried jointly by several categories. Take shelf life: plastic film supplies barrier material, special-purpose packaging equipment supplies heat-sealing and sterilisation equipment, and special-purpose food and beverage equipment supplies the complete line; if any one of the three categories is missing, not a single bag of ambient-stable food can be made. Take damage tolerance: pressure vessels carry the pressure-bearing body, containers carry the pressure and stacking loads of transport, and metal and plastic packaging carry the seal at the consumer end; the four categories together form the chain this report discusses as "boundary reliability".
Third, the relationship between categories and capabilities is many-to-many. A metal packaging plant's products serve food and also chemicals; a knitwear plant makes both winter clothes and summer clothes. Categories are used only to locate supply, not to define capability.
For a buyer, the use of this table is to locate, not to rank. To judge whether a category has sufficient supply, whether a supporting base has formed, and whether there is a second supplier, look at the national total and the concentration; to judge whether a particular company can do the work, one must return to the individual enterprise and look at its products, processes, qualifications and delivery record. The former is a map, the latter is the site, and the two cannot replace each other.
One common misuse must also be avoided when reading this table: adding the sixteen figures together and treating the result as "the total volume of related manufacturing". This does not hold as a statistical measure. The same enterprise may belong to several categories at once — an enterprise making both woven and knitted garments, for example, is counted twice; the categories also overlap upstream and downstream, and film and packaging containers, or down and down products, are not parallel categories. This report therefore gives no total, and does not recommend that readers add the figures up themselves.
Chapter 9: Geographic Distribution: Concentration in Five Provinces and Nearby Supporting Supply
Put the province columns of Table 2 together and a stable combination appears: Zhejiang, Jiangsu, Shandong, Hebei and Guangdong.
Of the sixteen categories, Zhejiang enters the top five sixteen times, Jiangsu fifteen, Shandong thirteen, and Hebei and Guangdong twelve each; below them come Anhui with five, Henan with three and Fujian with two. That five provinces appear in the top five of almost every category is not a coincidence.
The explanation behind this is supporting-supply density. On a complete chain, if any one segment — materials, forming, testing, certification, packaging, logistics — is missing, the finished item cannot be delivered; a place with low costs but an incomplete chain cannot take orders for the finished item. The longer the chain a product requires, the higher its demand for nearby supporting supply.
Take a down jacket. It requires outer fabric, lining, down-proof fabric, down, zippers, fasteners, sewing, down filling and testing. Down processing is concentrated in Henan, Anhui and Hebei; down product processing in Zhejiang; woven and knitted garments in Guangdong, Zhejiang, Jiangsu and Fujian. A garment factory in Zhejiang can source fabric, down-proof fabric, zippers and down-filling capacity within a few hundred kilometres; move the same order to a region with no light-textile base, and materials must be brought in from other provinces, with delivery dates and costs beyond control.
Take a penicillin production line. It requires fermenters, sterilisation equipment, filtration equipment, chromatography equipment, drying equipment, cleanroom equipment and packaging equipment, as well as a stable supply of active pharmaceutical ingredients. The supply of special-purpose pharmaceutical equipment is concentrated in Jiangsu, Zhejiang and Shanghai; chemical pharmaceutical ingredients in Shandong, Jiangsu, Zhejiang, Anhui and Hubei. The two distributions do not fully overlap, and between them lie the chemical industry base, energy and environmental treatment capacity — active pharmaceutical ingredient production requires stable utilities and reliable environmental facilities, and these conditions cannot be made up in a short period.
Take packaging. Plastic film is concentrated in Guangdong, Zhejiang, Jiangsu, Shandong and Hebei; special-purpose packaging equipment in Guangdong, Zhejiang, Hebei, Jiangsu and Shandong; the top five of the two largely overlap. Packaging is an industry of nearby supporting supply: rollstock is bulky and expensive to ship, so film plants, printing plants, bag-making plants and food plants often form a chain within a few hundred kilometres, and long-distance transport does not pay.
It should be added that beyond the five provinces there are still places with strong single-point positions. Henan in pressure vessels (118 enterprises), Anhui (209) and Hubei (196) in active pharmaceutical ingredients, and Henan (196) and Anhui (195) in down processing all enter the top five of their respective categories. These places do not lead in total volume, but in a particular sub-product they may be the main source of supply. Reading distribution by province yields only a first-layer conclusion; to reach a specific product category, one must go back and search by the specific product term.
It should be noted that concentration is not monopoly. Beyond the top five of the sixteen categories there are still large numbers of enterprises; this report lists only the top five. Concentration indicates supporting-supply density, not that other places cannot do the work.
Behind the provincial figures there is a further layer of county-level distribution. Within a province, capacity is often concentrated in a few counties and cities rather than spread evenly: stainless-steel kitchenware in Jieyang and Chaozhou, plastic household goods in Taizhou, household ceramics in Quanzhou and Chaozhou, down processing in a few counties of Henan and Anhui. Enterprise records can be located down to the county level, and on that basis a buyer judges not only which province to go to, but which county, and how far around it the supply can be assembled. This report lists only provinces in Table 2 because provincial figures are sufficient to support a judgement about supporting-supply density; at county level, one must check one product term at a time during a search.
Part IV: How to Ask When Buying
Chapter 10: Five Sets of Questions and Their Indicators
The reason the factory specification sheet is unsuited to answering these questions is that it is compiled on the premise of standard operating conditions. Standard conditions assume the equipment is used as instructed, the medium meets requirements and the environment is within the specified range; the specification sheet describes performance under that premise. The point of use rarely satisfies this premise: the medium may carry impurities, the environment may be humid and saline, operation may go wrong, maintenance may be postponed. The five capabilities describe precisely the performance after departure from standard conditions, so they can only be obtained through a different set of questions.
None of the five capabilities appears on a factory specification sheet, but all of them can be brought out by questions. Table 3 gives five sets of questions, the corresponding indicators, and the materials this report recommends verifying.
| Capability | What to ask | Corresponding indicator | Verification materials |
|---|---|---|---|
| Damage tolerance | What happens after a single-point failure, where is the isolation boundary, and can the boundary be detected | Design pressure, residual strength, leak rate, detection sensitivity | Design calculations, non-destructive testing reports, pressure and airtightness test records |
| Maintainability | How quickly a failure can be repaired, whether critical parts have spares, whether self-test is possible on site | Mean time to repair, mean time between failures, spare-parts fill rate, fault-isolation rate | Maintenance manuals, spare-parts lists and prices, training programmes, response-time clauses |
| Scale-up | What the scale-up is based on, how contamination is controlled, how cleaning and sterilisation are verified, and whether equipment or building comes first | Volumetric mass-transfer coefficient, power per unit volume, tip speed, sterility validation conclusions | Pilot-scale data, cases at the same scale, cleaning and sterilisation validation reports, building interface drawings |
| Shelf life | How shelf life is verified, how seals and leaks are checked, whether the retort's temperature-distribution records are kept | Water activity, F value, seal strength, leak rate | Accelerated test reports, heat-distribution and heat-penetration records, migration test reports |
| Environmental adaptability | Whether the use scenario is static or in motion, whether moisture-vapour transmission rate has been measured, what the down fill weight and fill power are | Thermal resistance, moisture resistance, moisture-vapour transmission rate, weather resistance | Test reports under identical test conditions, comparative data for the finished garment and the fabric, data before and after washing |
These five sets of questions do not require the buyer to understand all of the technology, but they do require knowing what to ask. Ask the right questions and the supplier will bring out data, reports and cases; ask the wrong ones and all one hears is "no problem" and "use it with confidence".
Two points need attention when using these five sets of questions. First, questions must be pinned to a specific object. Asking "is your equipment reliable" yields no useful answer; asking "what is the mean time to repair for this model, and does it count from the repair request or from the engineer's arrival" yields a checkable definition. Second, questions must match the scenario. For equipment installed on a remote hilltop, the repair time limit matters more than parameter precision; for packaging that faces consumers directly, seal strength is more likely to fail than barrier-layer thickness. The same supplier does not have the same pass line in the two scenarios.
For procurement projects that already have explicit technical requirements, these five sets of questions can serve as a supplementary checklist to the existing requirements; for projects with no written requirements yet, they can serve directly as the requirements themselves. Either way, before anything is written into the contract, confirm whether the supplier can provide verifiable materials rather than verbal assurances.
The measurability of an indicator determines whether a question can be put into practice. Mean time to repair, seal strength, moisture-vapour transmission rate and leak rate all have established test methods; they can be written into a contract and checked; expressions such as "good reliability" or "timely service" cannot be checked and can only be treated as intentions. Turning unmeasurable requirements into measurable indicators is what these five sets of questions actually do.
Chapter 11: How Capability Is Verified: Standards, Testing and Records
What the five capabilities share is that they are exposed only at the point of use, so verification can rest only on three things: standards, testing and records.
Standards deliver comparability. Thermal resistance, moisture resistance and moisture-vapour transmission rate each have their own test methods; GB/T 11048 and GB/T 12704 specify the test conditions, specimen dimensions and calculation methods, making it possible to compare results from different laboratories. For down, GB/T 17685 specifies the technical requirements for down and feathers, and GB/T 14272 is the product standard for down garments. Pressure vessels follow design-by-rule codes, with materials, design, manufacturing, and inspection and acceptance each covered in separate volumes. Retort pouches are produced under commercial sterility requirements, with sterilisation intensity converted through the F value.
Testing establishes whether the work was done. Seal strength must be measured, leaks checked, welds subjected to flaw detection, and the retort put through heat-distribution tests. The value of testing lies not in the report itself but in the fact that it turns "it was done" into a record that can be checked.
Records establish whether anything can be traced. Every inspection step has a standard, a record and a responsible person. Whether damage tolerance design holds depends on whether these records were really produced; whether shelf life can be delivered depends on whether a sterilisation curve exists for every batch; whether maintainability can be realised depends on whether the spare-parts list and training records are delivered with the equipment.
Only the three together give "verifiable capability" its meaning. Writing these three into the contract at the time of purchase is more useful than adding two more lines of indicators to the specification sheet.
The question of standard versions needs a separate mention. For the same performance, different versions of a standard may specify different specimen dimensions, test conditions and pass criteria, and the results cannot be compared directly. It is not enough to write "meets the national standard" in a procurement document; the standard number, year of issue and test conditions must be stated clearly, and the reports a supplier provides must show which version they are based on. This is especially visible in textiles: thermal resistance and moisture resistance follow one test-method system, and moisture-vapour transmission rate follows another, so comparing figures obtained by mixing the two methods leads to wrong conclusions.
Part V: Conclusion
Chapter 12: Five Measures That Never Appear in the Output Value Table
Put the five chapters together and five measures emerge.
The first is damage tolerance. After equipment has been hit and damaged, can it keep working? The corresponding design methods are compartmentation, isolation and sealing, at the cost of weight, volume, cost and inspection complexity.
The second is maintainability. After equipment breaks down, can it be repaired, how quickly can it be repaired, and what is needed to repair it? The corresponding design methods are accessibility, modularity, testability, spare parts, documentation and training; the corresponding measures are mean time to repair, mean time between failures and spare-parts fill rate.
The third is scale-up. Can something made in the laboratory be scaled up into stable factory output? The corresponding design methods are mass transfer, heat transfer, mixing, sterility, control and downstream processing; the corresponding criteria are the volumetric mass-transfer coefficient (kLa), power per unit volume and tip speed.
The fourth is shelf life. How long can food or medicine be kept at ambient temperature, and will it spoil in transit? The corresponding design methods are water activity, sterilisation intensity, barrier properties, sealing and testing; the corresponding measures are the F value, seal strength, leak rate and barrier performance.
The fifth is environmental adaptability. Can a product work normally under conditions of cold, heat, wind, water, dust, vibration and corrosion? The corresponding design methods are material selection, layer structure, surface treatment, sealing and breathability; the corresponding measures are thermal resistance, moisture resistance, moisture-vapour transmission rate and weather resistance.
These five measures have three things in common.
First, they are not written on the product's factory specification sheet. The specification sheet gives dimensions, material, power, precision and the certificate of conformity, and describes the state under standard conditions; these five describe the state under non-standard conditions, are exposed only at the point of use, and can be confirmed only through tests, verification and field data.
Second, they are all the result of trade-offs. Compartmentation costs volume, modularity adds connectors, scale-up has to sacrifice one mass-transfer indicator, shelf life costs taste or nutrition, and environmental adaptability costs weight or breathability. None of them is better the higher it is; each must match the mission scenario.
Take a concrete example. Given the same requirement of "durability", a pressure vessel and a down jacket achieve it by completely different routes: the former by increasing wall thickness, raising weld grades and tightening inspection, at the cost of weight and cost; the latter by raising the fabric's abrasion-resistance index, densifying the down-proof fabric and improving sewing, at the cost of hand feel and moisture transmission. Both routes can be inspected, but the items inspected differ, and so do the clauses that can be agreed in a contract. Treat "durability" as a single indicator for price comparison and only price is compared; break it into verifiable items and the differences can be compared.
Third, all of them can be brought out by procurement questions. The five sets of questions in Part IV correspond to these five capabilities.
The five measures are also coupled. A barrier layer thickened to improve shelf life makes the packaging harder to recycle and changes the feel when the bag is opened; modules and connectors added to improve maintainability add failure points and in turn affect damage tolerance; a higher stirring intensity for scale-up changes shear conditions and thereby affects product consistency. This coupling means the five capabilities cannot be optimised one by one; only a suitable value for each can be chosen simultaneously under a set of constraints. A buyer who demands the extreme value on every item usually ends up with a machine that is unsuitable on every item.
Chapter 13: Implications for Buyers and Suppliers
For buyers, there are three implications.
First, write capability into the technical requirements, not just parameters. Two machines with identical parameters may differ greatly in whether they can keep working after being knocked, frozen or misused. Setting out failure modes, isolation boundaries, repair time limits and verification methods is more useful than adding two more lines of precision.
Second, write the verification method into the contract. Test reports, validation records, spare-parts lists and training programmes are deliverables that can be agreed. What is not agreed will not be there at delivery.
Third, state the use scenario clearly. Static or in motion, dry or humid, ambient or extreme cold — these conditions determine the appropriate value of each of the five capabilities. A supplier who does not know the scenario can only deliver against generic specifications.
For suppliers, there are also three implications.
First, capability can become a point of differentiation. On the same industrial belt, a supplier that can provide validation data, spare-parts support and on-site training is harder to replace than one that only quotes a price.
Second, capability has to be recorded, or it cannot be replicated. One veteran master being able to repair something does not mean a whole shift can; one successful run does not mean every batch will succeed. Only when experience is written into documents, processes and inspection records does capability stay with the enterprise.
Third, the cost of capability has to be calculated clearly. Compartmentation, modularity, spare-parts stock and inspection records all add cost, and that cost will ultimately show up in the quotation. What a buyer squeezes out in price negotiations is often precisely these items that are not written on the specification sheet, and they are the very things that decide success or failure at the point of use.
The questions this report does not answer also need to be stated. First, what the average level of each of the five capabilities is in the industries of the two countries: this report has no comparable data and can give only individual cases and supply distribution. Second, the conversion relationship between capability and price: this report has not measured it, since the same damage-tolerant design adds very different proportions of cost to different products. Third, whether wartime practice can be transplanted directly into civilian procurement: this report has made only a logical analogy and no empirical test. All three require additional data and another study.
The common premise of the five capabilities is that the point of use is always more complicated than the laboratory. Only by acknowledging the complexity of the point of use do those indicators beyond the specification sheet have a place; and only when they are written into verifiable clauses at the time of purchase does manufacturing capability truly take hold.
Data Sources and Main References
The material for this report falls into three categories.
The first is public publications and memoirs. The first issue of Party Literature (Dang de Wenxian) for 2025 (whole number 229) carries He Huaikai and Wei Jingyuan, "A Study of Tunnel Warfare by the Chinese People's Volunteers in the War to Resist US Aggression and Aid Korea", pages 105 to 115; section 106 of Hong Xuezhi, Memoirs; and the North China Pharmaceutical Factory's factory-history story "Building the Plant in Three Years, Success on the First Trial Run".
The second is public reporting. "The CETC Presence in That War 70 Years Ago" (website of the State Administration of Science, Technology and Industry for National Defence), CETC 14's "Salute to 70 Years" series "China's First Radar Battalion", and "How Was New China's First Radar Battalion Established?" (Sina Military); reporting on the Shanghai Penicillin Laboratory by Changning District, Shanghai, and The Paper; a biography of Tong Cun in China Pharmaceutical News; and related articles in Past Events by China Science Communication and the Hongkou District Archives; Xu Ping, "Winter Uniform Support in the War to Resist US Aggression and Aid Korea", China National Defence News, 10 January 2025; Xu Ping, "Cotton-padded Clothes, Cotton-padded Clothes! Why Did the Volunteers at Changjin Lake Not Have Them?", PLA Daily, 2021; "Premier Zhou Instructed That Volunteers' Uniforms Must Use New Cotton", China Military Online; "Our Army Successfully Develops a New Type of Individual Self-Heating Food", China Military Online, 2017; "No Cooking Smoke Throughout the Exercise! Southern Theatre Command Army Explores a New Fast-Food Model for Field Catering Support", Ministry of National Defence website, 24 October 2020; and "Field Food Revealed", CCTV's Military Fans Worldwide, 18 January 2023.
The third is the Institute's enterprise records. The enterprise counts for the sixteen industry categories are compiled by middle class and small class of the national economic industry classification, covering only enterprises operating normally and excluding companies the platform has added from other sources. The counts are enterprise records, not industry output value, not output volume and not production capacity. The same enterprise may belong to several categories at once, and the figures in different rows cannot be added together. Data were extracted in October 2026.
The statements of engineering principle, including compartmentation and isolation, maintainability, fermentation scale-up, water activity and sterilisation, and thermal and moisture resistance, are public engineering common knowledge, and this report describes them only qualitatively. Standard numbers and titles follow the standards currently in force; test conditions may differ between versions, and in procurement the version agreed in the contract should prevail.